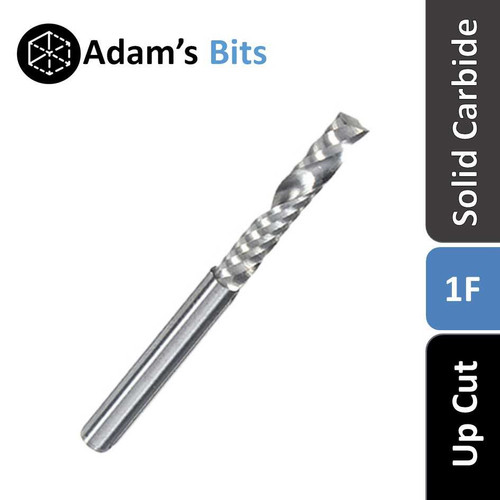
A 1 flute up cut carbide end mill is purpose-built for cutting plastics cleanly and cool. It runs a single cutting edge with a large, open flute, and the up-cut spiral pulls chips up and out of the cut as it works. That aggressive chip evacuation is exactly what plastics need — it keeps the cutting zone clear, stops chips from being re-cut, and carries heat away before it can melt or re-weld the material. The result is a smooth, gummy-free finish in materials that would quickly melt or pack up behind a multi-flute bit.
The single flute is the key. With only one edge, each revolution takes a bigger, cleaner chip and leaves far more room to clear it — so the bit can run fast without generating the friction heat that melts acrylic and polycarbonate. Because the up-cut geometry lifts chips upward, it leaves the cleanest edge on the bottom face of the workpiece and clears deep slots without packing. The trade-off is the mirror image of a down-cut bit: chips exit on top, so it needs good hold-down and can leave a rougher top edge on thin or delicate stock.
Suitable for
- Acrylic (cast and extruded / PMMA) and polycarbonate (Lexan)
- ABS, HDPE, nylon, acetal (Delrin), PVC and most machinable plastics
- Foams, and soft timbers where fast chip clearance matters
Not ideal for
- Plys— the up-cut can fray or chip the top surface; use a down-cut bit instead
- Thin, unsupported sheet without solid hold-down — the upward pull can lift or chatter the material
- Hard metals and steel — this tool is optimised for plastics and soft materials, not ferrous cutting
Adam’s Tips
The most common problem cutting plastic is melting, and the fix is almost always counter-intuitive: if the edge is gummy or the chips are re-welding, increase your feed rate or drop your RPM. A single flute relies on a decent chip load — a bigger chip carries the heat out of the cut with it, while a slow feed just rubs and melts. Aim to keep the chips flowing and clearing, not powdering.
Because an up-cut bit pulls chips (and the material) upward, good work holding is essential — use a vacuum table, clamps, or tape-and-glue on thin sheet to stop it lifting.
| Feeds and Speeds - 1 Flute for Plastics mm per minute | |||
| Plastics/Wood | |||
| Item Code | Description | Soft | Hard |
| 0.8-3.175-SP-1F-3 | 0.8mm x 3.175mm x 3mm 1F | 650 | 350 |
| 1-3.175-SP-1F-4 | 1mm x 3.175mm x 4mm 1F | 800 | 400 |
| 1.5-1/8-SP-1F-6 | 1.5mm x 3.175mm x 6mm 1F | 1,250 | 650 |
| 2-1/8-SP-1F-8 | 2mm x 3.175mm x 8mm 1F | 1,700 | 850 |
| 2-1/8-SP-1F-12 | 2mm x 3.175mm x 12mm 1F | 1,450 | 750 |
| 2.5-1/8-SP-1F-12 | 2.5mm x 3.175mm x 12mm 1F | 2,050 | 1,050 |
| 1/8-1/8-SP-1F-12 | 3.175mm x 3.175mm x 12mm 1F | 3,050 | 1,550 |
| 1/8-1/8-SP-1F-17 | 3.175mm x 3.175mm x 17mm 1F | 2,450 | 1,250 |
| 1/8-1/8-SP-1F-22 | 3.175mm x 3.175mm x 22mm 1F | 1,950 | 1,000 |
| 4-4-SP-1F-17 | 4mm x 4mm x 17mm 1F | 3,800 | 1,900 |
| 4-4-SP-1F-22 | 4mm x 4mm x 22mm 1F | 3,000 | 1,500 |
| 6-6-SP-1F-17 | 6mm x 6mm x 17mm 1F | 9,350 | 4,700 |
| 6-6-SP-1F-22 | 6mm x 6mm x 22mm 1F | 7,500 | 3,750 |
| 6-6-SP-1F-32 | 6mm x 6mm x 32mm 1F | 4,800 | 2,400 |
| 6-6-SP-1F-52 | 6mm x 6mm x 52mm 1F | 1,950 | 1,000 |
| 3.175-6.35-SP-1F-17 | 3.175mm x 6.35mm x 17mm 1F | 2,450 | 1,250 |
| 4-6.35-SP-1F-22 | 4mm x 6.35mm x 22mm 1F | 3,000 | 1,500 |
| 6.35-6.35-SP-1F-22 | 6.35mm x 6.35mm x 22mm 1F | 8,650 | 4,350 |
| 8-8-SP-1F-22 | 8mm x 8mm x 22mm 1F | 16,550 | 8,300 |
| 10-10-SP-1F-22 | 10mm x 10mm x 22mm 1F | 34,300 | 17,150 |
| 12-12-SP-1F-32 | 12mm x 12mm x 32mm 1F | 43,650 | 21,850 |
| Revolutions per minute 16,000RPM | |||
| 100% width per cut slotting | |||
| Depth per cut Diameter x 1 | |||
Sizes and dimensions
1 Flute UP CUT Carbide End Mill (for Plastics) comes in 43 sizes. Pick yours from the size options above; the dimensions for each are listed here.
| Cutting diameter | Shank | Cut length | SKU |
|---|---|---|---|
| 0.8mm (1/32") | 3.175mm (1/8") | 3mm | 0.8-3.175-SP-1F-3 |
| 1mm | 3.175mm (1/8") | 4mm | 1-3.175-SP-1F-4 |
| 1.5mm | 3.175mm (1/8") | 6mm | 1.5-1/8-SP-1F-6 |
| 2mm | 3.175mm (1/8") | 8mm | 2-1/8-SP-1F-8 |
| 2mm | 3.175mm (1/8") | 12mm | 2-1/8-SP-1F-12 |
| 2.5mm | 3.175mm (1/8") | 8mm | 2.5-1/8-SP-1F-8 |
| 2.5mm | 3.175mm (1/8") | 12mm | 2.5-1/8-SP-1F-12 |
| 3.175mm (1/8") | 3.175mm (1/8") | 8mm | 1/8-1/8-SP-1F-8 |
| 3.175mm (1/8") | 3.175mm (1/8") | 12mm | 1/8-1/8-SP-1F-12 |
| 3.175mm (1/8") | 3.175mm (1/8") | 17mm | 1/8-1/8-SP-1F-17 |
| 3.175mm (1/8") | 3.175mm (1/8") | 22mm | 1/8-1/8-SP-1F-22 |
| 3.175mm (1/8") | 3.175mm (1/8") | 32mm | 1/8-1/8-SP-1F-32 |
| 3.175mm (1/8") | 6mm | 17mm | 3.175-6-SP-1F-17 |
| 3.175mm (1/8") | 6.35mm (1/4") | 17mm | 3.175-6.35-SP-1F-17 |
| 4mm | 4mm | 12mm | 4-4-SP-1F-12 |
| 4mm | 4mm | 17mm | 4-4-SP-1F-17 |
| 4mm | 4mm | 22mm | 4-4-SP-1F-22 |
| 4mm | 4mm | 32mm | 4-4-SP-1F-32 |
| 4mm | 4mm | 42mm | 4-4-SP-1F-42 |
| 4mm | 6mm | 17mm | 4-6-SP-1F-17 |
| 4mm | 6.35mm (1/4") | 22mm | 4-6.35-SP-1F-22 |
| 4.67mm | 6mm | 17mm | 4.67-6-SP-1F-17 |
| 5mm | 6mm | 17mm | 5-6-SP-1F-17 |
| 5mm | 6mm | 22mm | 5-6-SP-1F-22 |
| 5mm | 6mm | 32mm | 5-6-SP-1F-32 |
| 6mm | 6mm | 12mm | 6-6-SP-1F-12 |
| 6mm | 6mm | 17mm | 6-6-SP-1F-17 |
| 6mm | 6mm | 22mm | 6-6-SP-1F-22 |
| 6mm | 6mm | 32mm | 6-6-SP-1F-32 |
| 6mm | 6mm | 42mm | 6-6-SP-1F-42 |
| 6mm | 6mm | 52mm | 6-6-SP-1F-52 |
| 6.35mm (1/4") | 6.35mm (1/4") | 22mm | 6.35-6.35-SP-1F-22 |
| 6.35mm (1/4") | 6.35mm (1/4") | 32mm | 6.35-6.35-SP-1F-32 |
| 6.35mm (1/4") | 6.35mm (1/4") | 42mm | 6.35-6.35-SP-1F-42 |
| 8mm | 8mm | 22mm | 8-8-SP-1F-22 |
| 8mm | 8mm | 32mm | 8-8-SP-1F-32 |
| 8mm | 8mm | 42mm | 8-8-SP-1F-42 |
| 8mm | 8mm | 52mm | 8-8-SP-1F-52 |
| 10mm | 10mm | 22mm | 10-10-SP-1F-22 |
| 10mm | 10mm | 32mm | 10-10-SP-1F-32 |
| 10mm | 10mm | 52mm | 10-10-SP-1F-52 |
| 12mm | 12mm | 32mm | 12-12-SP-1F-32 |
| 12mm | 12mm | 52mm | 12-12-SP-1F-52 |
Buying guide: Best Router Bits for Acrylic and Plastics · Up Cut vs Down Cut vs Compression · MultiCam Tool Equivalents · Why Router Bits Break
Frequently asked questions
Why use a 1 flute bit for plastics?
The single large polished flute lifts chips out fast, so heat leaves with the chip instead of melting the plastic. Multi-flute bits re-cut chips and can weld acrylic back into the slot.
Which plastics can it cut?
Acrylic, polycarbonate, ABS, HDPE, nylon, acetal and PVC. It also works well in softwood and XPS foam.
Does it work on plywood or steel?
It is not recommended for plywood or steel. For aluminium and hard plastics, the 1 Flute Up Cut DLC is the better choice.
Why are my thin sheets lifting?
An up cut pulls material upward. Use solid hold-down such as double-sided tape, masking tape and super glue, or clamps, and tabs on small parts.
What speed should I run?
16,000 rpm is a good start. Set the feed with the calculator at feeds.endmill.com.au.
84 Reviews Hide Reviews Show Reviews
-
Great milling bit
I have been having trouble with cutting soft plastics and getting build up on the tip. These bits work beautifully and no buildup on the tip.
-
Very happy with my selection of uncut bits
It done everything I needed to on my CNC machine and good finish
-
Single Flute Upcut
Been using these cutters for while now very happy with them
-
3mm EM
Great cutters, great results using them with HDPE and Polycarb
-
1 flute upcut bit
Good quality bits delivered quickly. I will continue to buy from Adam's Bits.
-
1 flute up cut carbide end mill for plastics.
The end mill is sharp, its dimensions are as described and it is robust. I have used it several times and have gotten excellent results and so far no loss of sharpness.
-
Up cut end mill for plastics
Worked very well with a clean cut.
-
Sigle Flute carbide up cutter for plastics
This is a great cutter, we can run higher feed-rates than our previous tools and the cutters are much less expensive. Highly recommended.
-
Single flute upcut Endmill
Great cutters, work well with hard and soft plastics